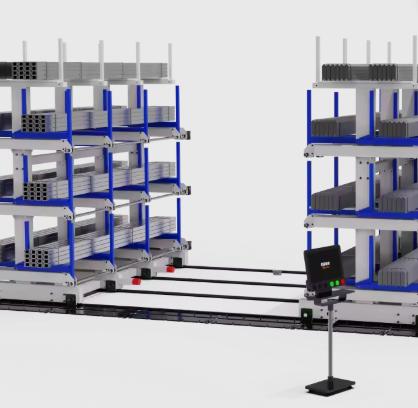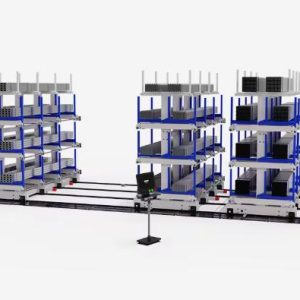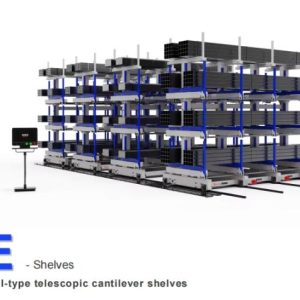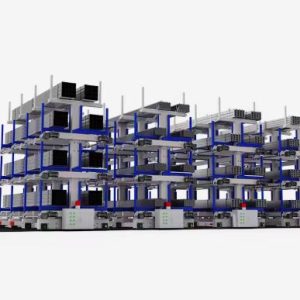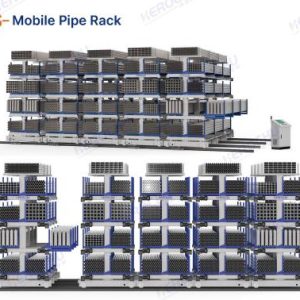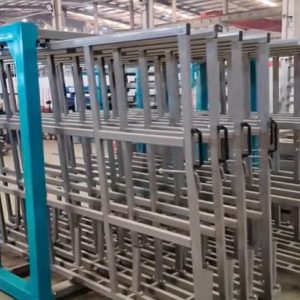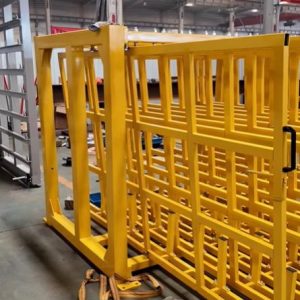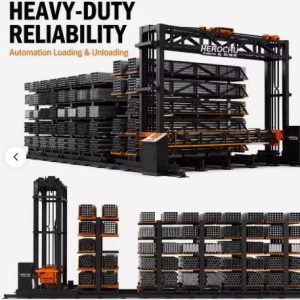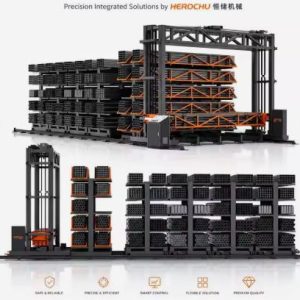
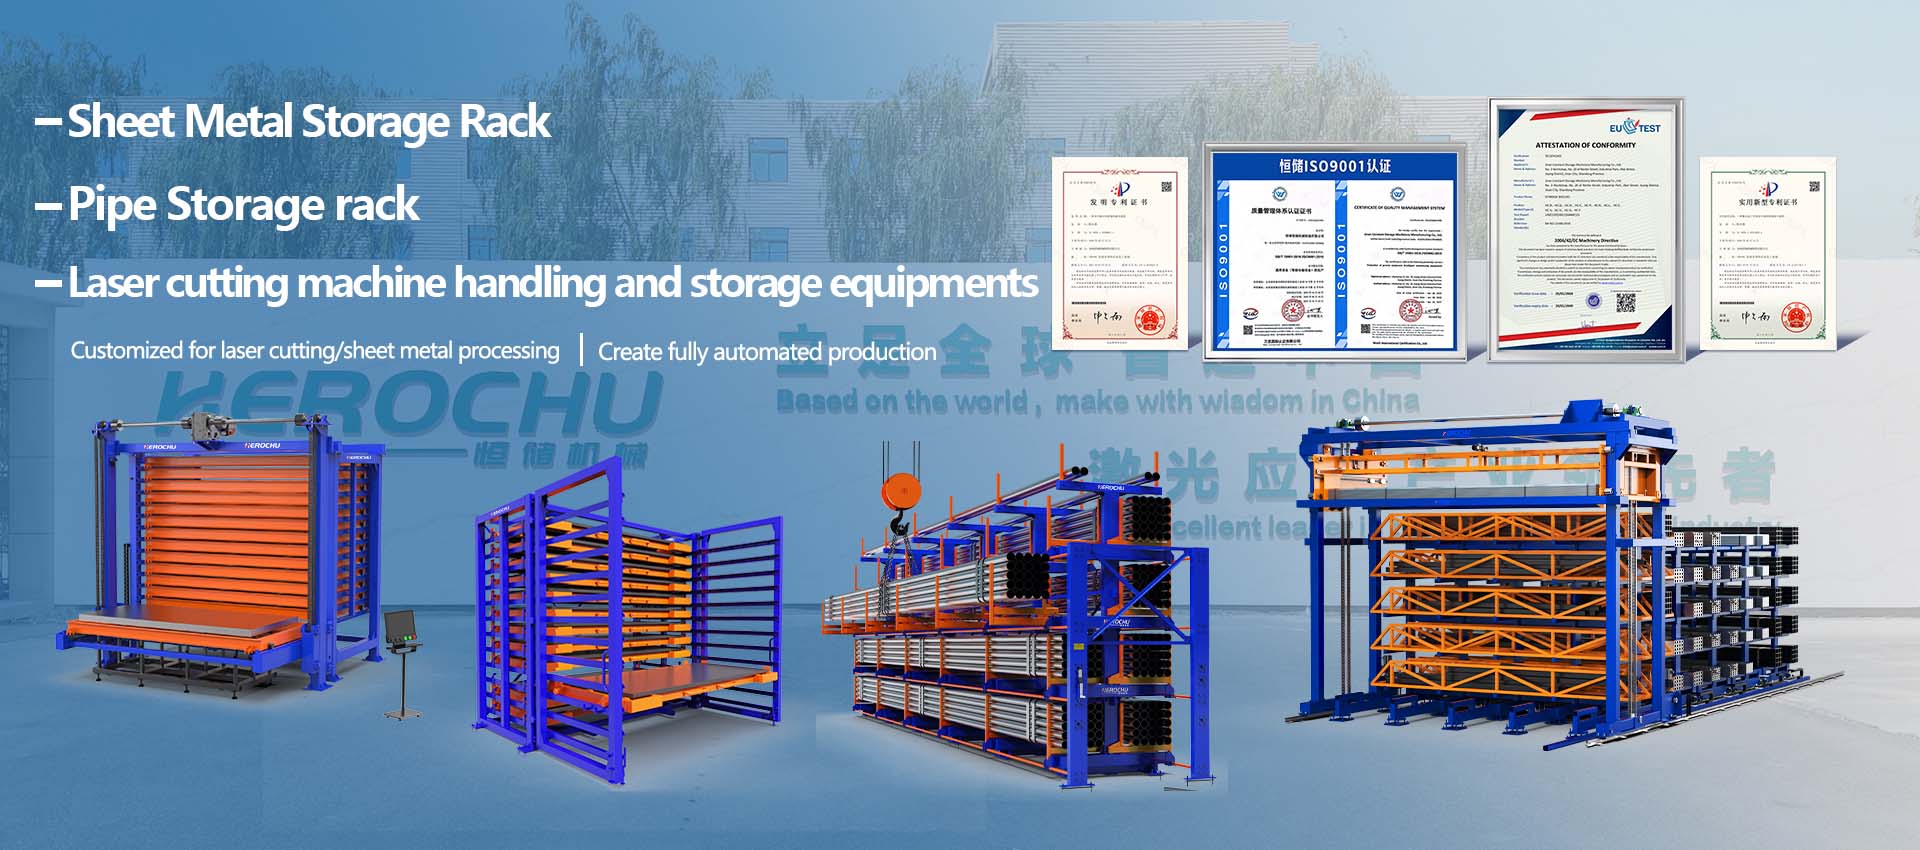
Industrial facilities storing steel pipe, structural tubing, and bar stock face a common structural problem: the heavier the inventory, the more demanding the storage requirements become. Standard cantilever racks can handle moderate loads, but when per-level weight ratings climb into the multiple-ton range, structural integrity, drive mechanism durability, and operator safety all require a purpose-built solution. The Herochu heavy duty mobile pipe system is engineered specifically for these high-load conditions, combining reinforced steel construction with motorized rail-guided mobility.
Load Ratings Built for Industrial Service
Each level of the Herochu mobile pipe system is rated for substantial weight capacity. The HC-G6053EM-5 model supports up to three thousand kilograms per level across five customizable layers, designed for six-thousand-millimeter pipe lengths. The HC-G9055EM-7 and HC-G12065EM-7 models both carry five thousand kilograms per level, handling nine-thousand and twelve-thousand-millimeter pipes respectively across seven rack towers each. The HC-G12065EM-7 features six layers rather than five, providing additional vertical storage tiers for facilities managing large-diameter or thick-wall tubing.
These load ratings reflect static capacity under normal operating conditions, with structural safety margins engineered into the column profiles, base frames, and cantilever arms. Q235B high-strength steel forms the primary structural framework, selected for its yield characteristics under sustained heavy loading and its performance in welded connections subject to dynamic forces during rack movement.
Motorized Drive Architecture
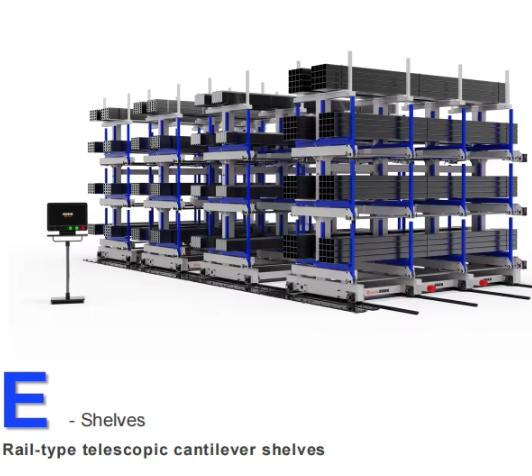
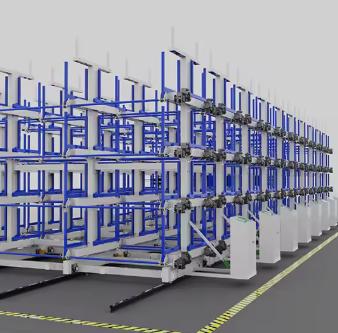
Moving several tons of steel pipe along a floor rail requires a drive system capable of delivering consistent torque without overstressing the structural frame. The Herochu system uses a linear guide rail paired with chain drive transmission to move rack groups along the ground track. Carriage speed is set at twenty-seven millimeters per second, providing controlled acceleration and deceleration that prevents load shifting during transit. Rack traveling speed ranges from one to five meters per minute, adjustable based on the total moving mass and the distance between closed and open positions.
The chain drive configuration offers practical advantages over belt or direct-drive alternatives in heavy-load applications. Chains maintain positive engagement with drive sprockets under high tension, resist elongation better than belts under sustained load cycling, and can be serviced or replaced without dismantling the rack base structure. A Siemens PLC unit manages drive commands, integrating speed control, position feedback, and safety interlock functions into a single control architecture.
Electric-Assisted Material Discharge
Loading and unloading heavy pipe bundles manually is both inefficient and hazardous. The Herochu system incorporates electric-assisted material discharge, reducing the physical force required to move pipe bundles onto and off of storage arms. Combined with overhead crane or vacuum lifter access, this allows a single operator to manage material handling tasks that would otherwise require multiple workers and extended handling time.
Vertical lifting speed is rated at nine meters per minute, with inlet and outlet speed at twelve meters per minute. These rates keep material flow consistent with typical crane cycle times, preventing bottlenecks at the storage face during peak retrieval periods.
Rail System and Structural Distribution
The floor-mounted rail serves two functions in the Herochu system: it guides rack movement and it distributes the total storage weight across a continuous structural path. Rather than concentrating load through isolated base plates into small patches of floor concrete, the rail spreads weight along its full length. This distribution reduces point-loading stress on warehouse floor slabs and improves overall structural stability when racks are fully loaded and in motion.
Rails can be floor-attached for surface mounting or ground-embedded for flush installation, depending on facility requirements and floor construction. Surface-mounted rails are faster to install and allow relocation if storage layouts change, while embedded rails provide a flush floor surface that simplifies forklift and personnel movement across the storage area.
Manufacturing Quality and Service Support
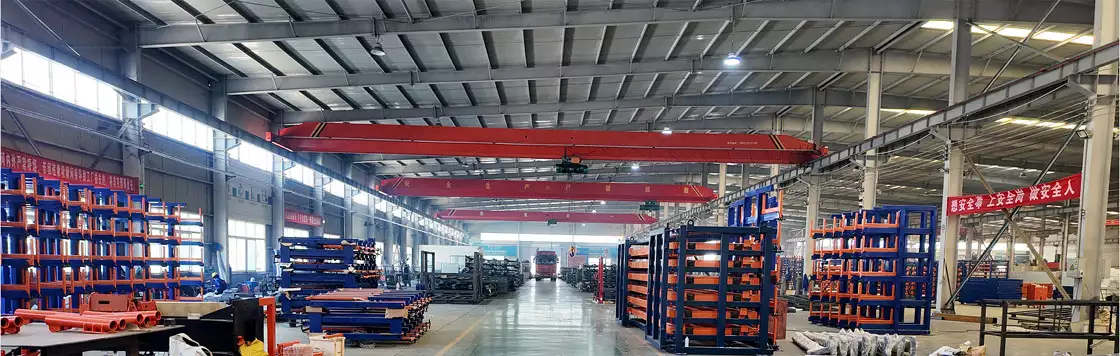
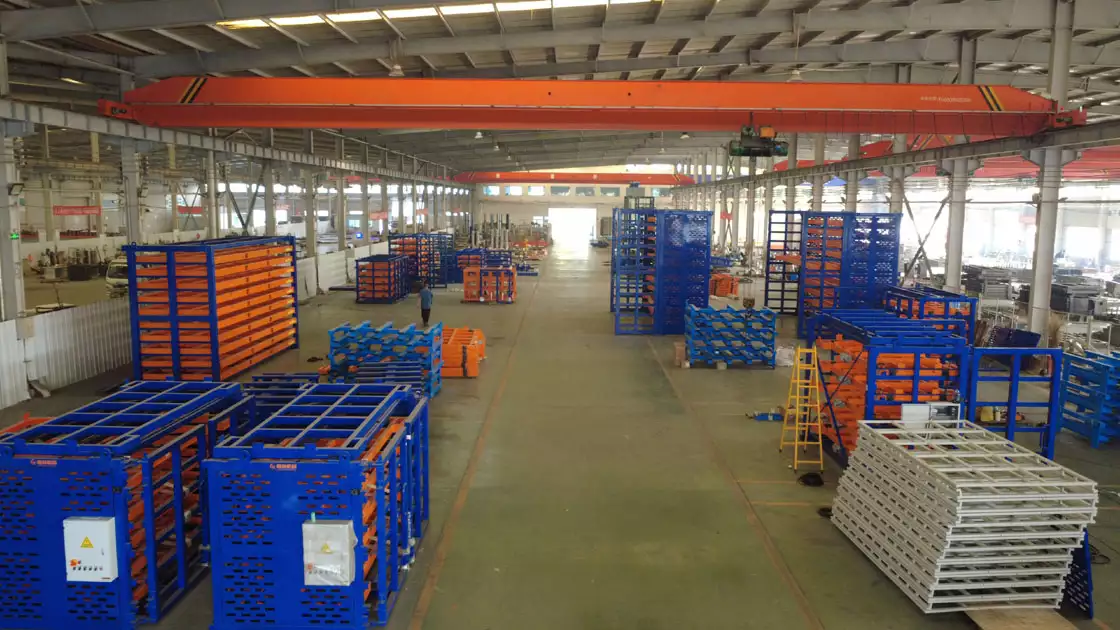
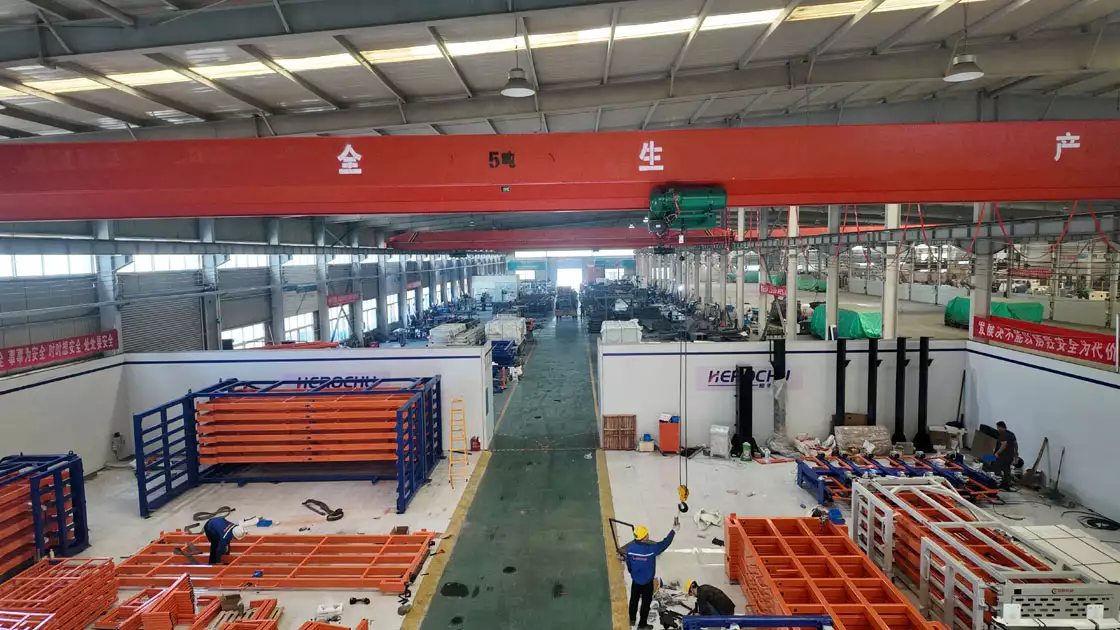
Herochu manufactures each heavy duty mobile pipe system to order, controlling every stage from steel cutting and welding through surface treatment and final assembly. Custom dimensions, color specifications, and layer configurations are available to match specific operational requirements. CAD layout consulting helps facility planners position rails, determine rack group sizing, and integrate the mobile system with existing material handling workflows before fabrication begins.
For installations requiring commissioning support, Herochu offers on-site assembly and startup services to verify rail alignment, drive calibration, and control system operation under loaded conditions. This direct-manufacturer approach, backed by over fifteen years of industry experience, ensures that each system meets its specified load ratings and operating parameters rather than relying on third-party assembly that may compromise structural tolerances.